Fitkari Alum Powder About
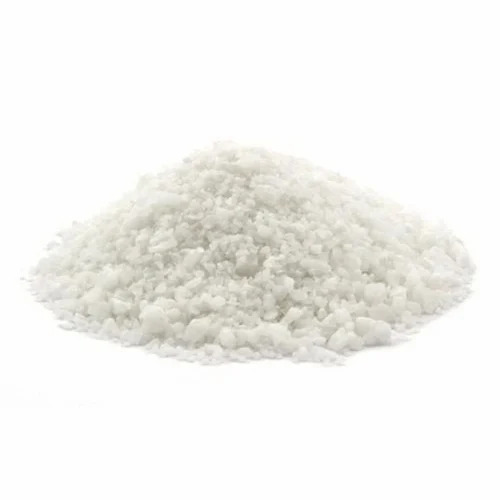
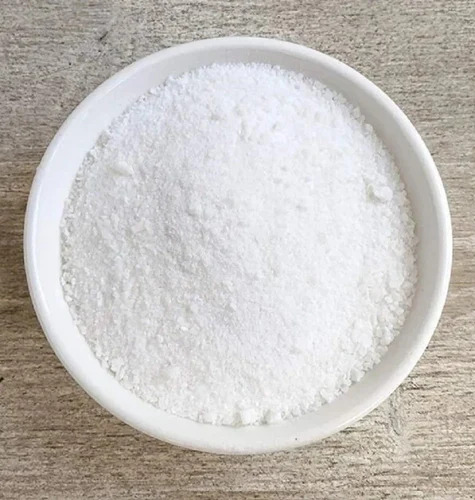
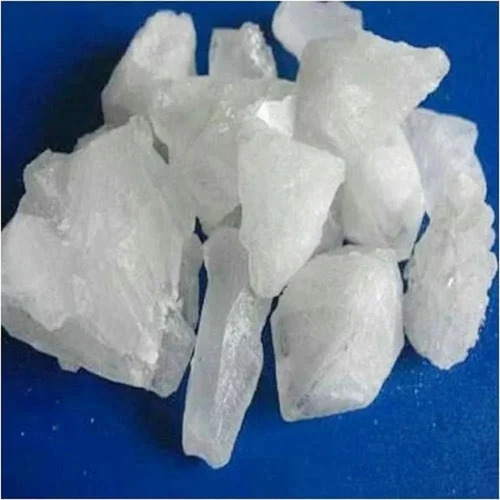
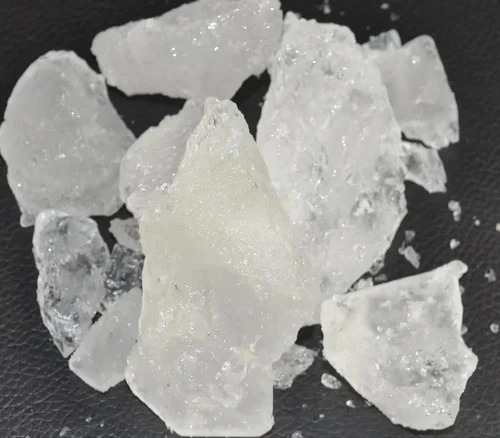
Our Fitkari Alum Powder is a top-tier, best-selling industrial product, offered at the lowest price for the highest quality. With its pure, easy-to-dissolve white crystals, this product exceeds 99% purity and meets IS: 260/1976 standards. Packaged in durable 50KG plastic bags, it is perfect for water purification, industrial processes, and aftershave. Spotlight on its monoclinic structure, free-flowing consistency, and low moisture content, making it the best choice for professionals seeking reliability, safety, and performance. Non-toxic and odorless, this granular or fine powder guarantees seamless application.
Unmatched Usage, Applications & Advantages of Fitkari Alum Powder
Fitkari Alum Powder excels in water purification, ensuring safe and clear water for various industries. Its use extends to aftershaves due to its astringent properties, and it is instrumental in various chemical industrial processes. Other applications include textile finishing and paper manufacturing. Competitive advantages include its high solubility, non-toxic nature, and stable monoclinic crystalline form. With IS: 260/1976 compliance, this product stands out for reliability and consistency in demanding industrial environments.
Packing Details, Exchange Opportunities & Cost Considerations
Each sale package of Fitkari Alum Powder comes in robust 50KG plastic bags, ensuring minimal expenditure on repackaging or storage. The exchange process is seamless with our FOB port located conveniently in India, making domestic sale transactions swift and efficient. Our highly rated product is available across India's main domestic markets, delivering exceptional value at a competitive sale price without compromising on quality. Optimal packaging preserves the free-flowing granular structure for efficient industrial use.
FAQ's of Fitkari Alum Powder:
Q: How is Fitkari Alum Powder typically used in water purification?
A: Fitkari Alum Powder acts as a superior coagulant, making it highly effective in removing suspended particles and impurities in water treatment plants, thus ensuring clear and safe water.
Q: What are the main industrial benefits of using high purity Fitkari Alum Powder?
A: With greater than 99% purity and a stable monoclinic structure, it enhances process efficiency in applications like textile sizing, paper manufacturing, and aftershave formulations, offering reliable, safe, and consistent results.
Q: When should Fitkari Alum Powder be added during water treatment processes?
A: It is best added during the pre-filtration stage, where its astringent properties and solubility allow it to bind impurities, resulting in efficient sedimentation and improved water clarity.
Q: Where can buyers source Fitkari Alum Powder in bulk quantities?
A: Buyers can source it directly from manufacturers and suppliers in India, with delivery facilitated through main domestic markets and FOB port exchange for convenience and cost-effectiveness.
Q: What packaging ensures the safe and easy handling of Fitkari Alum Powder?
A: Fitkari Alum Powder is offered in robust plastic bags weighing 50KG each, maintaining the product's free-flowing, granular structure and protecting it from moisture during storage and transport.




 Send Inquiry


 Send Inquiry
 Send Inquiry
